Abrasive Jumbo Roll Manufacturer: What Sets the Best Apart?
2026-09-21
Abrasive jumbo rolls might look like simple products on the surface, but ask any production manager who has chased a wandering splice or fought inconsistent grain shedding—suddenly, the manufacturer behind the roll becomes the most important supplier in the plant. In this guide, we break down the non-negotiables, from backing uniformity to tension control, and highlight how SHENZHEN SUN ABRASIVES tackles the demands that others miss.
Raw Material Choices That Separate Sharp from Average
The difference between a blade that holds its edge and one that dulls after a few uses often comes down to the steel's carbon content and how it's paired with alloying elements. High-carbon steels like 1095 or O1 can reach a finer, more stable edge because their carbide structure is tighter and more uniform. By contrast, softer stainless blends with excessive chromium and low carbon tend to roll or blunt quickly, even if they resist rust better on the surface.
Heat treatment matters just as much as the raw composition. A skilled maker can take a mid-tier steel and, through precise quenching and tempering cycles, push its edge retention well beyond what the spec sheet suggests. Conversely, even a premium powder metallurgy steel underperforms if the austenitizing temperature is off or the temper is rushed. The real separator is not the label on the billet but how the raw material's potential is unlocked through controlled thermal processing.
What separates sharp from average is rarely a single magic ingredient. It's the deliberate selection of raw materials that balance hardness, toughness, and grain refinement. Blades that combine a fine-grained matrix with a modest amount of hard vanadium or niobium carbides tend to sharpen easily yet resist abrasive wear. These choices, made before the first grind, determine whether a tool feels alive on the stone or becomes another forgettable piece of steel.
Coating Consistency You Can Measure, Not Just Claim
Most coating suppliers talk about consistency, but few hand you the numbers. We track viscosity at multiple shear rates, film build across a full panel, and gloss readings from edge to edge. If a batch drifts outside the agreed range, it gets flagged before it reaches your line—not after.
Our lab records dry film thickness with calibrated gauges and cross-checks surface texture under a profilometer. These aren't one-off samples; every production run carries a measurement log you can request. The result is less rework and fewer surprises when you switch batches.
What you get is not a promise that the coating “should” behave. You get the actual viscosity curve, DFT map, and gloss delta. If the numbers don't match the spec, we don't ship. That's the difference between claiming consistency and proving it.
Custom Roll Widths Without the Custom-Tooling Wait
Standard slitting and sheeting operations force you to choose between stock widths that may not fit your process and costly custom tooling with lead times that stall production. Our approach eliminates that trade-off by using adjustable, modular cutting systems that let you dial in exact roll widths on the fly. No new dies, no waiting for tooling revisions—just precise widths when you need them.
This flexibility comes from a combination of precision-guided blades and quick-change cassette setups that can be reconfigured in minutes. You gain the ability to run short batches or trial new dimensions without committing to expensive, permanent tooling. The result is a supply chain that responds to your actual consumption patterns instead of forcing you into predetermined sizes.
For converters and manufacturers who regularly shift between product specs, this means fewer roll changes, less trim waste, and the freedom to optimize every run. You get the performance of a custom width without the hidden cost of tooling storage, maintenance, or the delays that typically accompany custom orders.
Inspection Steps That Don't Just Check Boxes
Most inspection routines die by becoming a hunt for initials and dates. To get real value, start each walkthrough with one simple change: put the checklist face down for the first ten minutes. Watch how material actually moves, where people pause, which tools are improvised. That observation, before any box is ticked, tells you more than a hundred signed forms.
Next, turn at least one requirement into a live test. If the standard says a gauge is checked daily, watch someone perform that check instead of asking if it was done. Ask the person doing the work what would make the step easier or more reliable. Often the gap isn't negligence but a procedure that no longer matches the real process.
Finally, write findings the way you'd explain them to a colleague on the next shift. Avoid vague notes like "needs attention" and record what you saw, why it matters, and what would correct it. That kind of note builds a trail that helps the next inspection, instead of just proving that today's boxes were filled.
Technical Support That Understands Your Line Speed
When you're dealing with connection issues, the last thing you need is a support agent reading from a generic script about resetting your router. Our team is trained to look at the actual throughput numbers from your line, not just guess based on your plan's advertised speed. That means if your upload is degrading while download stays fine, we focus on upstream signal levels instead of wasting your time with irrelevant checks.
Slow speeds can be caused by anything from a faulty splitter to congestion on a specific upstream channel. We map out your modem's reported modulation profiles, error counts, and SNR history before making a single recommendation. You won't hear us tell you to restart your device twice unless we've already ruled out line noise, packet loss patterns, and node saturation on your street.
Most support centers treat every connection as if it's the same. We read your line rate, packet retransmission stats, and bufferbloat results before suggesting anything, because a 500 Mbps fiber line with latency spikes needs a completely different fix than a 50 Mbps copper loop with intermittent sync. That's the difference between getting your issue solved on the first call and going through four useless troubleshooting rounds.
Transit-Ready Packaging That Prevents Roll Damage
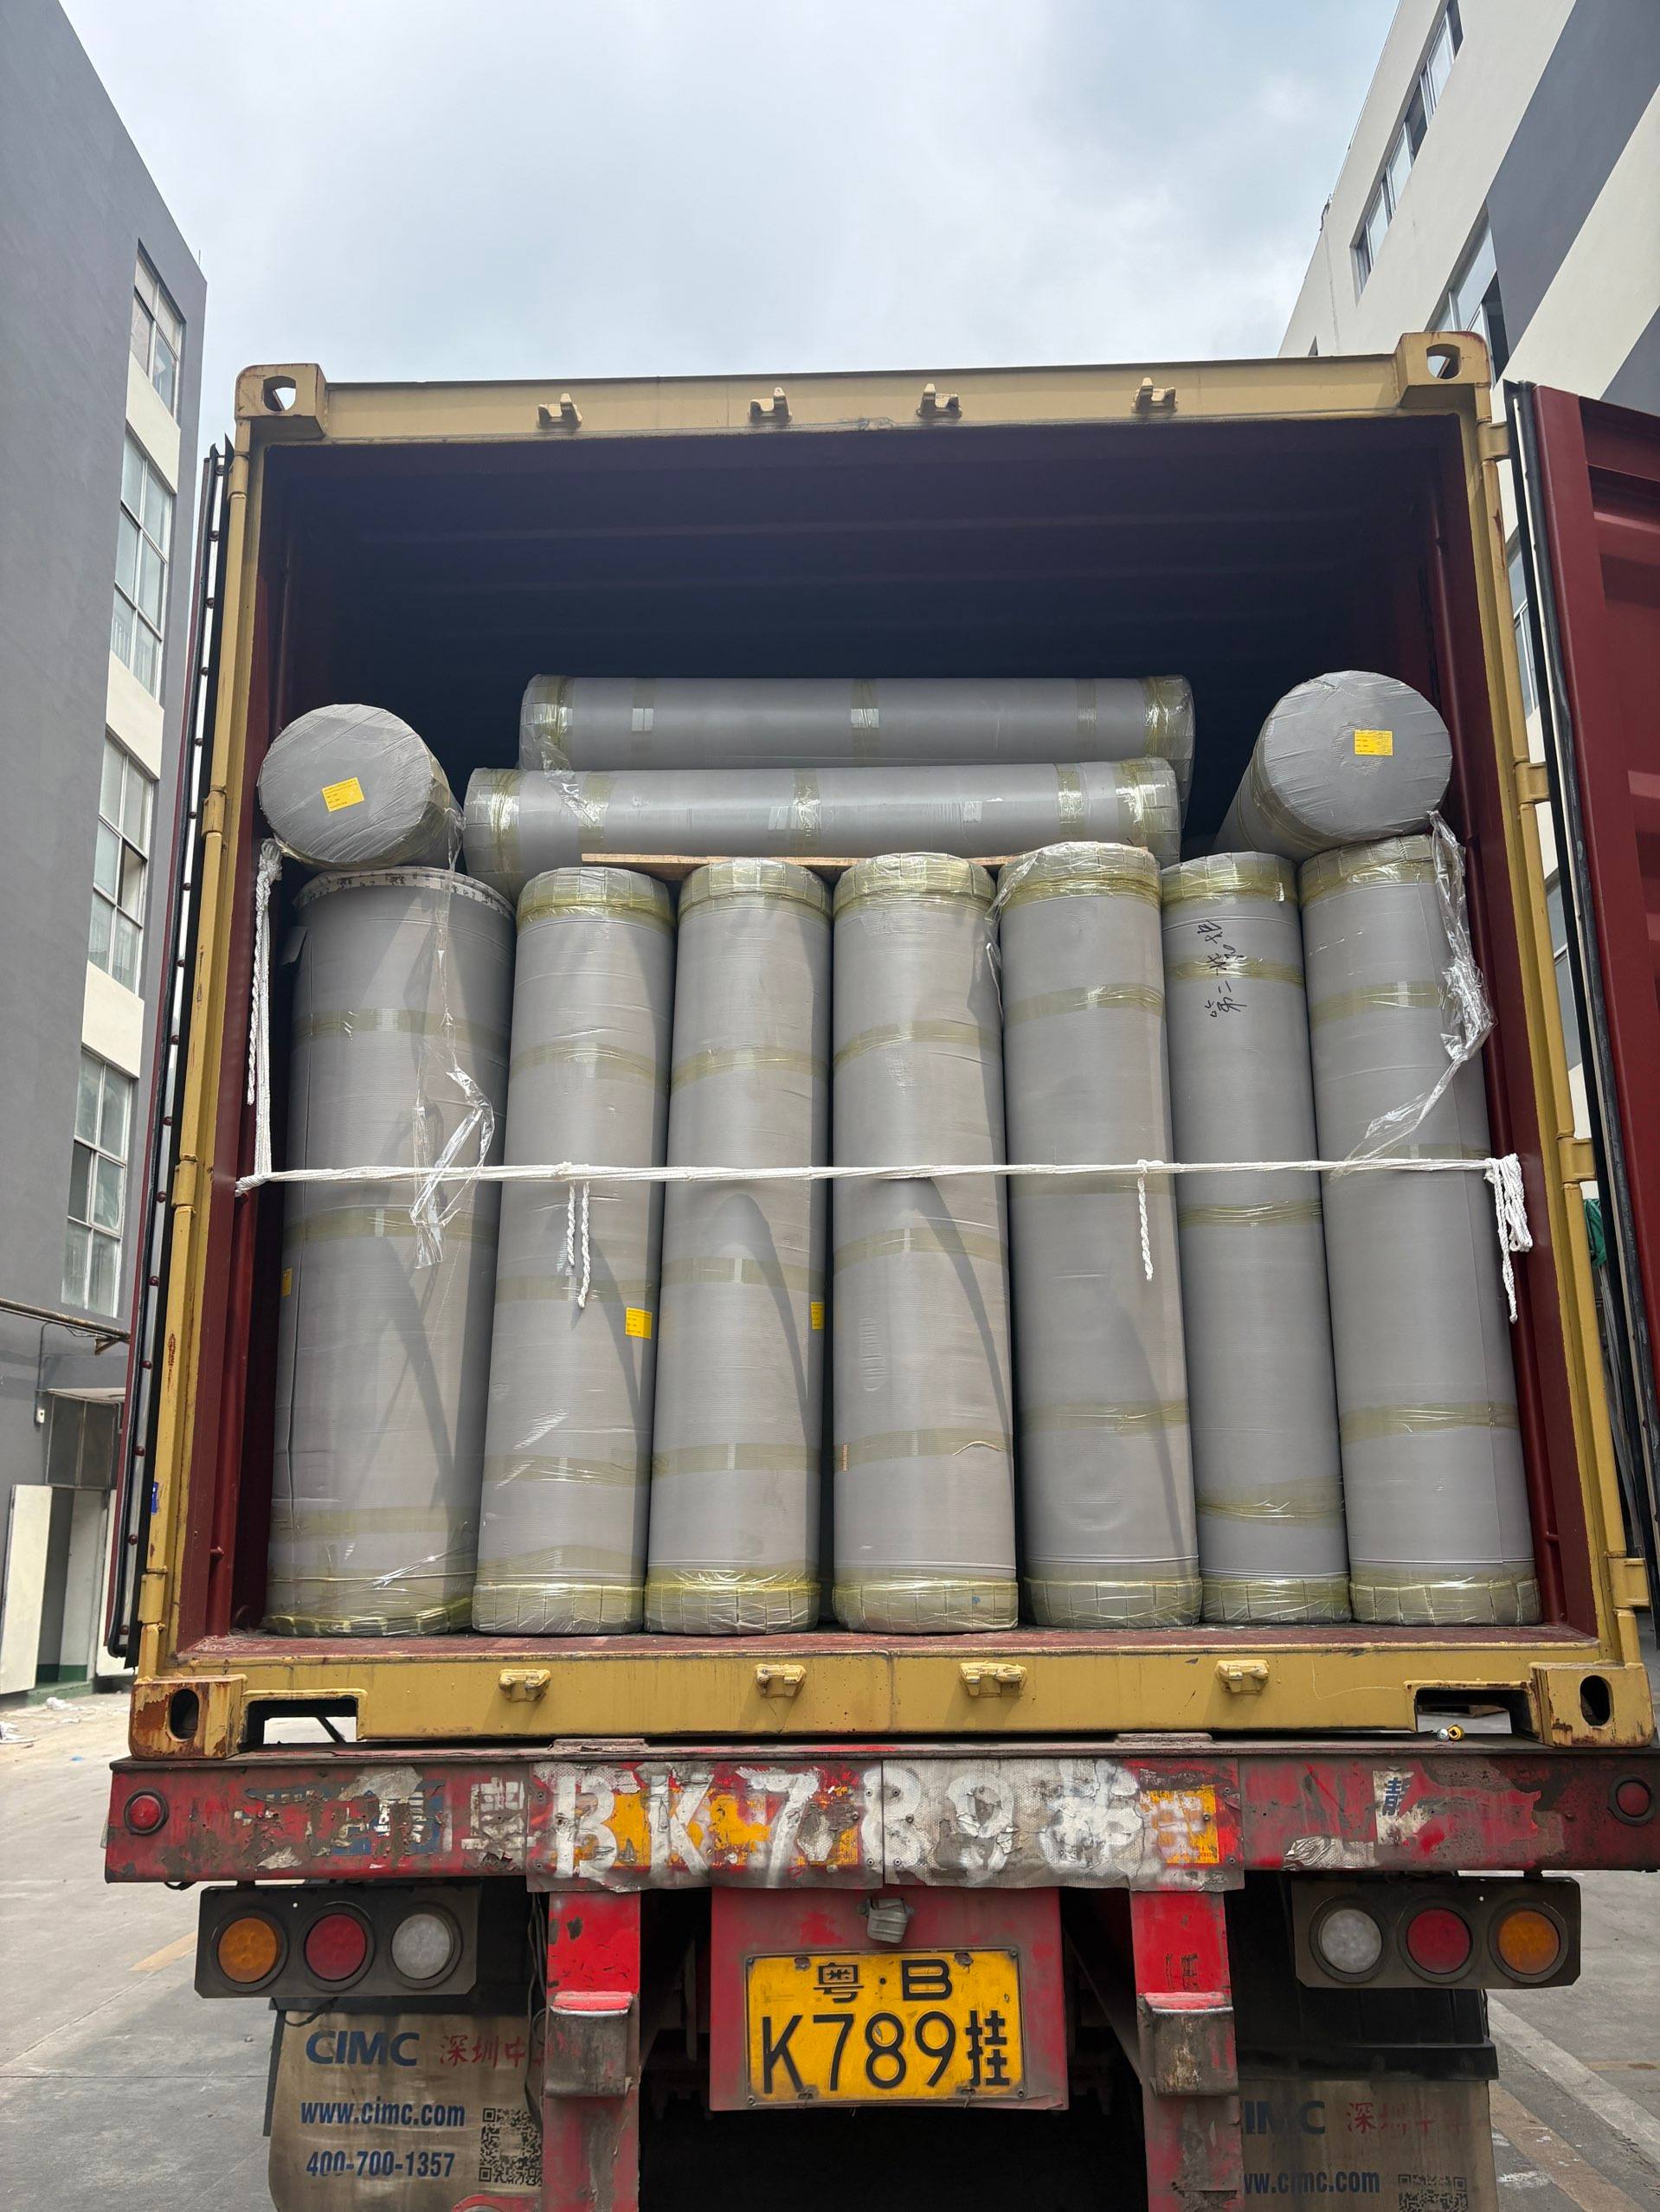
Rolls rarely sit still inside a container. Vibration, braking, and rough handling turn every mile into a test of restraint. Our packaging starts with custom-cut cradles and chocks that match the exact diameter and weight of your roll stock, so the core takes the load instead of the edges. High-density foam liners and reinforced end caps absorb lateral shifts before they reach the material surface.
The outer layer is where most damage goes unnoticed until unboxing. We use multiwall corrugated sleeves with a water-resistant barrier that keeps humidity and road spray from weakening the roll face. Steel-belted edge protectors are positioned at the two-o'clock and ten-o'clock contact points, where forks and straps typically bite in, distributing pressure evenly across the circumference.
Every pallet is then wrapped in a compression film that pulls inward rather than just covering the top. This keeps the roll from creeping toward the container walls during long hauls. Before any shipment leaves, we run a tilt-and-impact simulation based on the actual route profile, adjusting the blocking pattern until the roll stays within a 2 mm tolerance from its original position.
FAQ
They typically run a combination of peel adhesion tests, wet and dry flex tests, and high-speed slitting trials on every master roll. The best ones also log viscosity and gel time for each resin batch, so any deviation can be traced before the roll ships.
Wrinkles usually come from uneven tension during winding or moisture pickup in storage. Good manufacturers use closed-loop tension control on the winder, monitor core moisture content, and wrap rolls in vapor-barrier film. Some even add a slight crown to the winding drum to keep the web flat.
For wide belt sanding, polyester and heavy cotton blends dominate because they resist stretching and edge fraying. Paper backings are cheaper but fail fast under high tension. A knowledgeable manufacturer will ask about your machine's tension range and recommend a backing with the right elongation at break.
They use gravure or roller coating heads with automatic gap control, plus beta gauges or X-ray sensors that scan across the web every few seconds. If coating weight drifts outside a narrow band, the line slows down or alarms. That data is stored per roll, so you can request a coating profile certificate.
Not necessarily. A very heavy butt joint can create a hard spot that telegraphs through the sanded surface. The best manufacturers match joint thickness and hardness to the backing, often using a skived or zigzag lap joint that keeps the caliper nearly flat. They also test joint breaking strength under both dry and wet conditions.
Ask if the manufacturer stores master rolls in climate-controlled rooms and whether they acclimate rolls before slitting. Abrasive backings, especially paper and cloth, can change dimension by 2-4% between 20% and 80% relative humidity. Top suppliers keep converting areas below 50% RH and measure moisture in the backing before coating.
Look for in-house grain mixing and electrostatic coating capability. A supplier that only buys pre-coated rolls cannot adjust grit distribution for your finish requirements. The best ones can tweak the blend, open or closed coat, and even apply a supersize layer to reduce loading on softwoods or paints.
Conclusion
The best abrasive jumbo roll makers don't start with generic grain—they select minerals for fracture behavior under your exact pressure and belt speed, blending aluminum oxide, ceramic, or zirconia to match whether you're grinding stainless, wood, or composites. That sharp-versus-average gap shows up immediately in cut rate and heat buildup. Coating consistency is where many fall short; superior manufacturers run closed-loop weight checks across the full width, keeping grain density within tight tolerances so your sanding belt doesn't wander or leave patchy finishes. And when your line calls for non-standard widths, the right partner slits to size from in-stock parent rolls rather than forcing you into long tooling lead times or order minimums.
Inspection shouldn't just be a checklist—it means tension-testing splice strength, scanning for pinholes or voids under high-speed cameras, and verifying backing flexibility before rolls ship. Technical support matters most when you're pushing line speeds; the best teams ask about your conveyor speed, contact wheel hardness, and airflow cooling before recommending a product, not after. Finally, transit-ready packaging separates reliable suppliers from the rest: reinforced cores, moisture-barrier wrap, and edge protectors that survive bumpy freight keep the roll dimensionally stable and free of edge damage, so what arrives at your dock performs exactly like the sample you approved.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn