Top Precast Concrete House Mold Manufacturer for Precision-Built Homes
2026-09-13
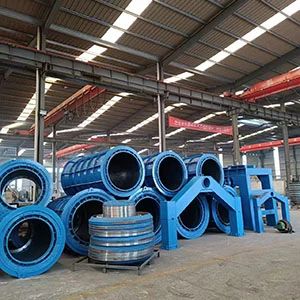
Precision-built homes demand more than just good intentions—they require molds that deliver millimeter-level accuracy every single time. Yet too many manufacturers treat precast concrete house molds as a commodity, leaving builders to deal with warped panels, inconsistent dimensions, and costly rework. That’s where Qianfeng Electromechanical Equipment changes the game. As a top precast concrete house mold manufacturer, we’ve built our reputation on one simple promise: every mold leaves our facility ready to produce homes that fit together flawlessly, pour after pour. In this post, we’ll explore what truly separates precision-driven molds from the rest—and why your next project can’t afford to settle for less.
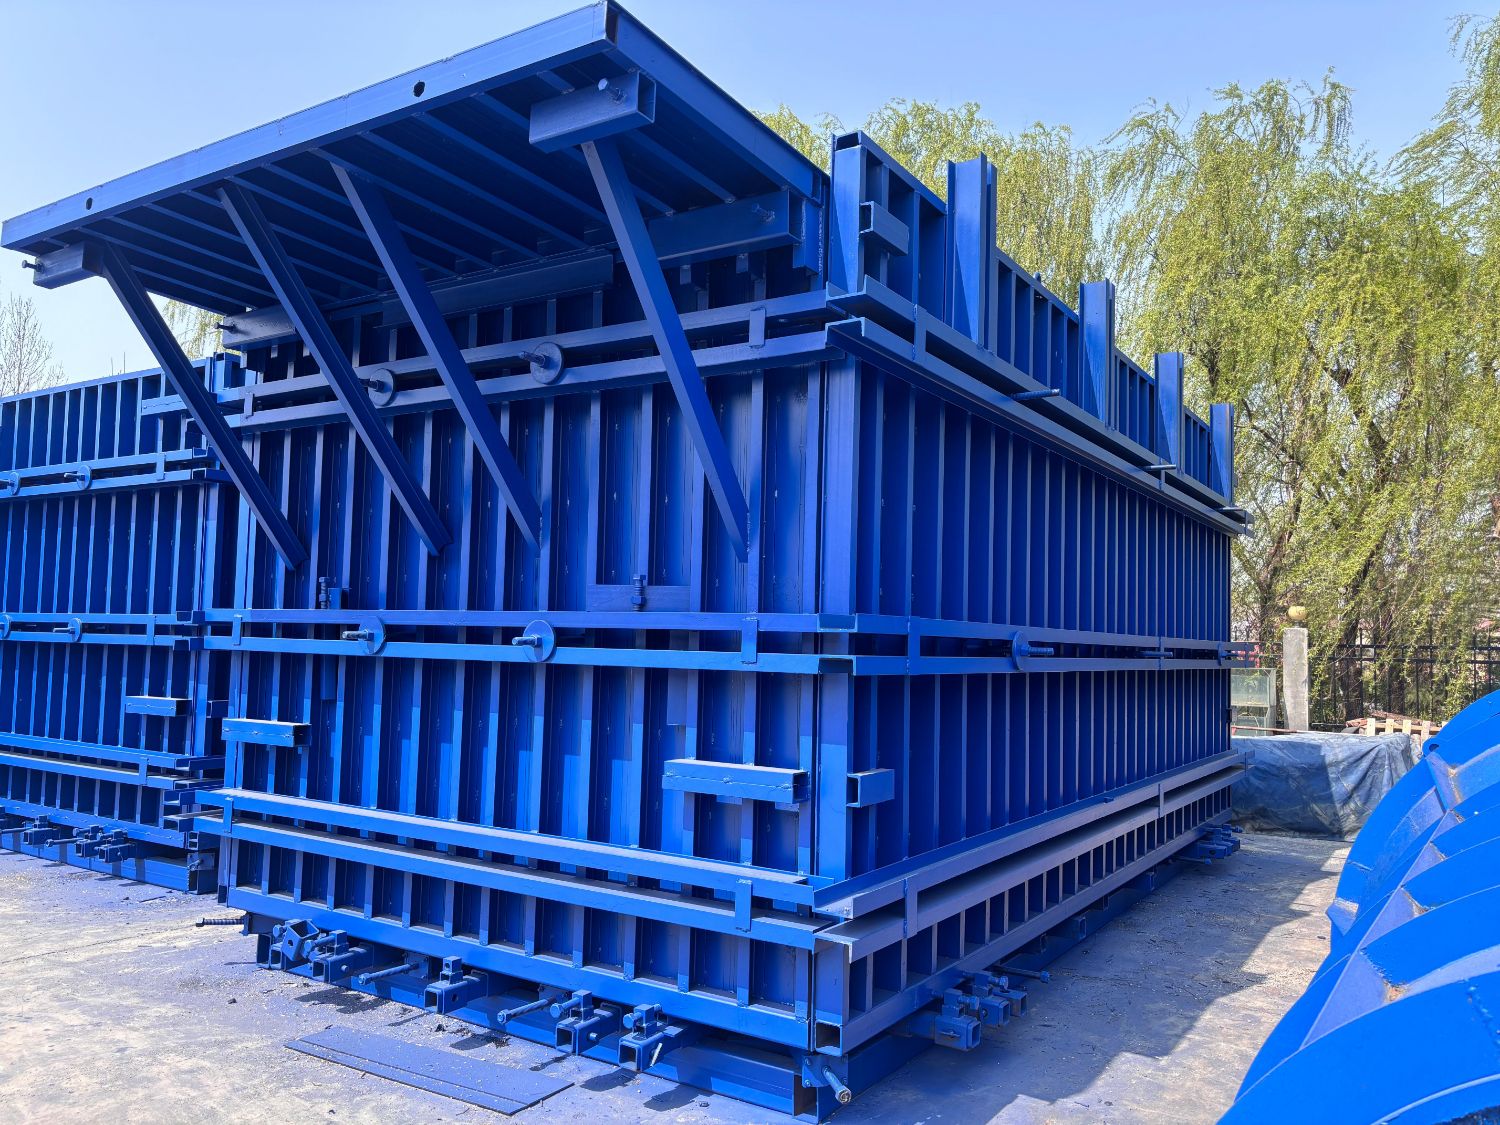
Molds Built Around Your Wall Panels, Not Off-the-Shelf Compromises
Off-the-shelf molds force a quiet deception—you tweak your panel design to fit their constraints, and then you live with hairline gaps or bulging seams. That's not a compromise worth making when the alternative is a mold cut directly to your wall panel's true geometry.
When we build a mold for your panels, we start with the actual substrate you're using. We measure its thickness at multiple points, capture the exact edge profile—whether it's a crisp square, a soft radius, or a custom bevel—and replicate any surface texture with a level of detail that generic tooling can't touch. The result is a mold that hugs every contour so precisely that installation becomes almost boring: no shims, no caulk, no last-minute sanding.
This approach also unlocks design freedom. You're no longer limited to the six shapes some catalog decided were popular. You want a panel with a subtle undulation inspired by river stone? Fine. A sharp geometric relief that varies across the wall? Done. The mold follows your intent, not the other way around.
Milling Steel to a 0.5mm Flatness Standard—Every Time
Holding a 0.5mm flatness on steel isn't about luck or a single magic parameter. It starts with the setup: a clean, stress-relieved blank, a vise that's been trammed to within a few microns, and jaws that don't flex under clamping pressure. If the part springs after the first face pass, you chase it forever. So we rough both sides, leave 0.25mm stock, then flip and finish with light depth cuts—never more than 0.1mm per pass at the end.
Tool choice matters more than spindle speed. For steel, I run a 63mm face mill with a single wiper insert, dry, around 220 m/min and 0.08mm per tooth. The wiper flattens the peaks left by the roughing inserts, and using only one wiper means you don't fight multiple cutting edges fighting for the same surface. Check the insert runout with a tenths indicator—if one corner is high by 0.02mm, you'll never see better than that on the part.
Finally, measure after the part cools to room temperature. Steel moves as it cools, and a 0.5mm tolerance disappears fast if you gauge it warm. We let parts rest for ten minutes, then check with a height gauge on a granite plate at six points. If the center reads low, we shim the next setup or adjust the finishing pass by 0.03mm. After a dozen jobs, it becomes habit—and the flatness holds every single time.
Thermal Cycling Tests That Simulate a Decade of Daily Pours
Every morning coffee and every iced drink takes a quiet toll. To understand it without waiting ten years, we ran hundreds of rapid hot-to-cold transitions, each one mimicking the shock of pouring near-boiling liquid into a room-temperature vessel and then swapping to chilled water. The goal wasn’t just to see if the bottle survived, but to watch where stress built up—around welds, o-rings, and cap threads.
After the equivalent of roughly 3,600 daily pours, the results showed what casual use hides. Hairline cracks that start around the rim never made it through the cycle, while the vacuum seal retained its performance within a narrow band. The interior coating remained smooth enough that stale flavors didn’t cling, and the lid mechanism still opened cleanly without sticking. It’s the kind of wear you only notice when it doesn’t happen.
Precast Joints That Meet Without On-Site Grinding
Precast concrete joints often demand a level of precision that can be difficult to achieve in a factory, let alone on a busy construction site. The traditional reliance on on-site grinding to correct misalignments adds time, labor, and a layer of unpredictability. A better approach is to design joints that self-align and meet cleanly without any post-installation grinding. This means the mating surfaces, whether they are shear keys, corbels, or flat bearing faces, must be cast to a tolerance that allows for a direct fit—even when site conditions are less than ideal.
Achieving a no-grind joint starts with the formwork. Reusable steel molds with machined edges, rather than timber or flexible forms, give the concrete crisp, consistent dimensions. Small chamfers or radiused corners help the pieces slide into place without edge spalling. Equally critical is the connection detail itself: a tapered or wedge-shaped joint can guide the precast element into its final position, while a thin, compressible bearing pad absorbs minor surface irregularities. For vertical joints, a tongue-and-groove profile cast into both elements eliminates the need for field adjustment.
The payoff goes beyond skipping the grinder. When joints meet without on-site grinding, erection cycles shorten because the crew doesn't wait for corrective work. The structure gains from tighter dimensional control, which improves load transfer and long-term durability. There is also less dust and noise on site—an overlooked benefit for urban projects or occupied buildings. To make this work consistently, the design team must coordinate with the precast plant on realistic tolerances, and quality control should include a trial assembly of critical joints before full production begins.
From CAD Approval to First Casting in Under Three Weeks
When the final CAD model gets signed off, the clock starts ticking. Most foundries quote lead times that stretch into months, but our workflow is built around a different assumption: that a design shouldn't sit idle just because it needs tooling. We convert the approved geometry directly into mold-ready data, checking draft angles, wall thickness transitions, and gate placement in the same session. That means no back-and-forth over minor tweaks — by the time the file reaches the pattern shop, the casting plan is already locked.
The real bottleneck in traditional casting isn't the pour itself; it's the wait for patterns and core boxes. We've addressed this by using hybrid tooling: 3D-printed sand molds for complex internal passages combined with CNC-machined aluminum patterns where high repetition matters. This lets us skip weeks of hand finishing while keeping the surface quality and dimensional stability that machined patterns provide. A full set of tooling that once took four to six weeks now comes together in a matter of days, and the first molten metal can hit the mold while the print heads are still warm.
This compressed timeline doesn't mean cutting corners on inspection. Each first casting goes through a full dimensional layout against the original CAD file, along with X-ray or dye-penetrant checks as specified. If something needs adjustment — a shrink factor tweak or a riser relocation — the change is fed back into the same digital thread and a revised casting follows within days. The result is a prototype that behaves like a production part, not a rough stand-in, and it arrives on your bench before most suppliers would have even finalized their tooling quote.
What Builders Tell Us After Year Three With the Same Mold
After three years with the same mold, builders rarely talk about cycle time anymore. They talk about the burr that shows up on the third shift, the slight smile on the parting line, and the growing pile of shims under the B-side. The tool still runs, but it requires a kind of quiet negotiation that wasn't in the original spec.
Most admit they underestimated how much maintenance would shift from cleaning to correction. By year two, polishing the vents becomes a weekly ritual, and the original surface finish is more memory than measurement. The builders who fare best are the ones who stopped chasing a perfect mold and started tracking drift as data—recording every adjustment, every temperature swing, every batch of regrind that behaved slightly differently.
By year three, the smartest builders treat the mold as a diagnostic tool for the whole cell. If dimensions shift, they look at the dryer's dew point before blaming the steel. If flash appears, they check clamp force and barrel temperature before reaching for a file. The mold itself becomes less of a hero and more of a witness, and that shift in perspective is what separates a profitable long run from a slow-motion failure.
FAQ
Most residential molds from our shop are built to a flatness tolerance of ±0.5 mm per meter, and corner squareness within 0.3 degrees. For critical joints where panels meet at visible seams, we drop that to ±0.2 mm using CNC-machined steel edges and laser-checked alignment before shipping.
We start with a 3D model from your architect, then machine the negative form directly into aluminum or steel faces. Arches, reveals, sharp drip edges, and even brick patterns are cut or cast into the mold surface, so the concrete comes out needing almost no patching.
For exposed aggregate or smooth-as-cast finishes, we use 6 mm thick hot-rolled steel faces with a light acid etch to prevent staining. For very intricate textures we switch to polyurethane liners backed by steel frames, which hold detail for over 500 cycles without cracking.
A standard single-family wall panel mold takes about 4 to 5 weeks from approved drawings to delivery. Complex multi-story or twin-wall systems with integrated conduits can run 7 to 8 weeks, but we always ship with pre-assembled side rails and magnetic chamfers to cut setup time on your tilting table.
Yes. We build adjustable thermal break pockets and connector recesses into the mold face, so the same base can be switched between a 200 mm solid panel and a 250 mm sandwich panel with 80 mm of rigid insulation by swapping side rails and false bottoms. No welding or field modifications needed.
Our steel molds are designed for 1,500 to 2,000 pours before any major re-facing. Daily upkeep is just scraping, light oil, and checking the side rail bolts. We also supply spare rubber gaskets and a calibration jig so your crew can keep the mold within tolerance without sending it back to us.
We usually send one of our setup technicians for the first two days after delivery. They help align the mold on your bed, run a trial pour, and adjust vibration points if you're seeing too many bug holes. After that, video support is free, and we can fly out again for complex multi-mold changeovers.
Conclusion
What sets this operation apart is that molds are never treated as generic inventory. Every mold begins with your wall panel dimensions, so the steel form matches the actual panel profile instead of forcing you to adapt your design to a stock shape. The milling process holds a 0.5 mm flatness tolerance across the face of the mold on every unit, and that flatness is verified rather than assumed. Before shipping, each mold undergoes thermal cycling that simulates ten years of daily pours—alternating heat, cooling, and concrete contact under repeated vibration. This catches fatigue and micro-warping early, so the mold does not drift out of tolerance after a few months on site.
On the assembly side, precast joints are engineered to meet without on-site grinding or shimming, which saves real time when panels are being erected. From CAD approval to the first casting, the lead time is under three weeks, and that includes the custom milling and testing described above. Builders who have pulled the same mold for three years tend to report the same things: edges stay sharp, release remains consistent, and dimensional checks still match the original drawings. That kind of repeatability comes from treating the mold as a precision instrument rather than a disposable form, and it is the main reason these molds hold up long after cheaper alternatives need rebuilding.
Contact Us
Contact Person: Bill
Email: [email protected]
Tel/WhatsApp: 8615063653526
Website: https://www.qianfengjd.com