Vision Measuring Machine Brand: Which One Delivers the Precision Your Parts Demand?
2026-10-22
Every micron counts when your parts are on the line. Yet, with so many vision measuring machine brands claiming unmatched accuracy, how do you separate real precision from marketing noise? That’s the question we’re tackling head-on. Among the contenders, JATEN has been quietly earning a reputation for delivering measurements you can trust—but does it live up to the demands of your production floor? In this blog, we’ll cut through the specs and hype to find the brand that truly delivers the precision your parts demand. Stay with us.
When Microns Decide Your Scrap Rate, Paper Specs Stop Being Enough
In actual production, the difference between 350 and 360 microns doesn't show up on a spec sheet until the die cutter starts jamming and the waste bin fills with half-scored blanks. Paper specs list nominal caliper, but reel-to-reel variation and humidity-driven swelling push thickness outside tolerance in ways a single lab reading never catches. When your scrap rate climbs by double digits, that's the real specification being violated.
Operators have learned to trust their fingertips more than the datasheet. A stack that feels spongy on the feed table, or a fold line that cracks instead of creasing, tells you more about runnability than any ISO test. The problem isn't that specs are wrong—they're just too static. Microns shift with ambient moisture, press pressure, and even the age of the paper. If you only check against the mill certificate, you're reacting to scrap, not preventing it.
Temperature Drift on Your Shop Floor Is the Quiet Precision Killer
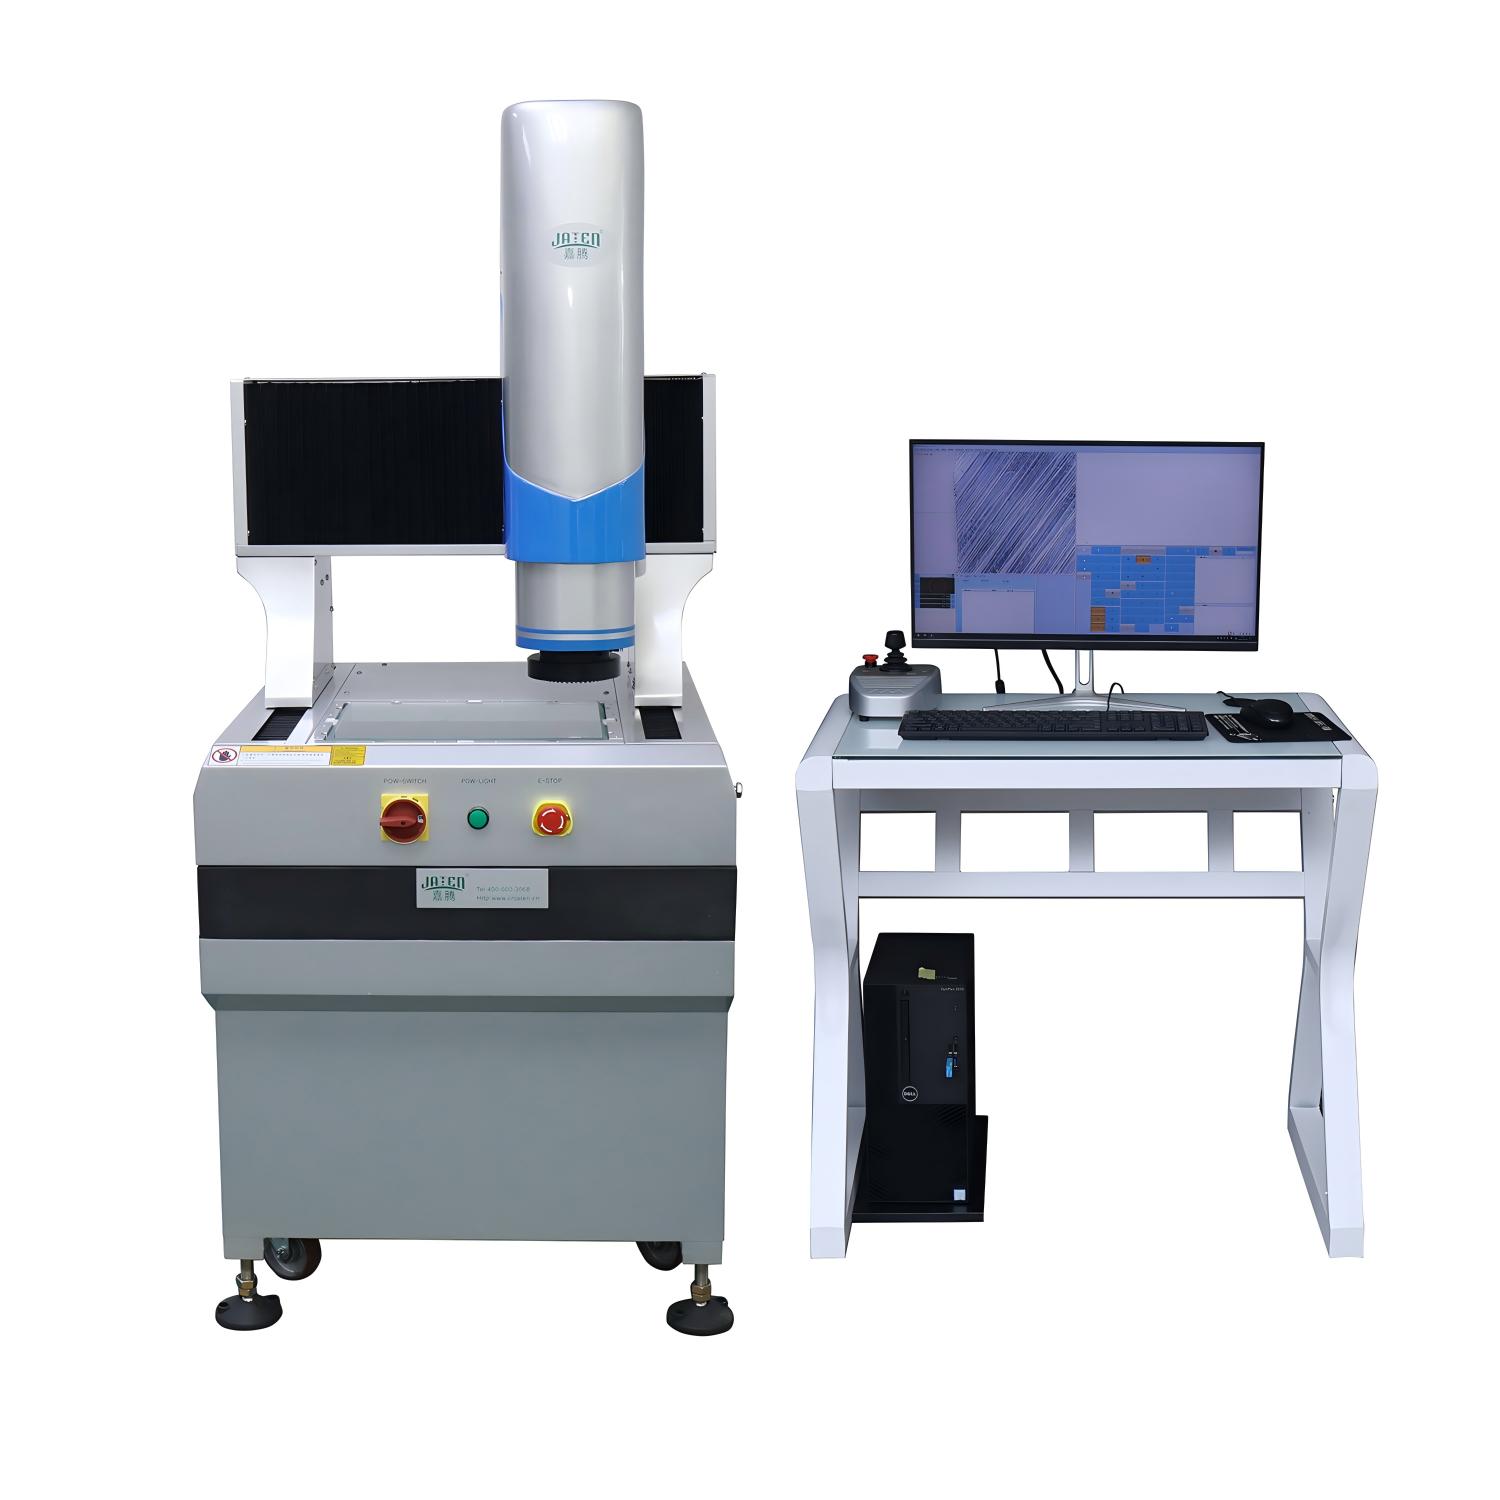
Walk through any machine shop mid-shift and you'll hear complaints about tool chatter, surface finish, or measurement mismatch. What rarely gets blamed is the slow, invisible creep of ambient temperature across the floor. A half-degree drift between morning startup and afternoon load can quietly undo the tightest tolerances, especially on long runs where metal expands and controllers chase phantom offsets.
The frustrating part is that temperature drift doesn't announce itself. You'll see a bore diameter drift out of spec by a few microns, tweak the offset, and then chase it again an hour later as the machine warms back up. It looks like an unstable process, but the real culprit is the shop's thermal environment—sun through a window, a door left open near the bay, or a coolant chiller cycling too aggressively. Precision dies by a thousand small thermal cuts.
Some shops fight back with climate zones, pre-shift warm-up cycles, and in-process probing that records temperature alongside dimensions. But unless you measure the drift itself—not just the part—you're adjusting blind. The quiet killer isn't the heat, it's the assumption that your shop floor holds still while your tolerances demand otherwise.
Software Is Not a Sidekick, Edge Detection Changes the Game
Edge detection has long been treated as a background process, something that quietly runs behind the scenes while the real action happens elsewhere. But that perspective misses what is actually going on. When software steps out of the shadows and starts making decisions at the edge, the entire flow of a system changes. It no longer waits for instructions from a distant server or a centralized brain. Instead, it reacts to the immediate environment, cutting down on the delays that quietly eat away at performance. This shift turns software into a primary actor, not a supporting one.
The difference becomes clear when you look at applications that depend on split-second timing. A camera that spots a defect on a production line cannot afford to send every frame to the cloud and wait for a response. The logic has to live where the action is. Once that happens, the role of the software changes. It stops being a passive tool and starts shaping how the hardware behaves in real time. The same principle applies to robotics, autonomous vehicles, and even mundane things like smart thermostats. In each case, edge detection gives the software a kind of agency that traditional architectures never allowed.
What really changes the game is that this approach redefines the relationship between code and hardware. Instead of treating the physical device as a dumb sensor and the software as a distant brain, edge detection collapses the distance. The code becomes part of the machine's reflexes. That means faster responses, lower bandwidth use, and systems that keep working even when the network drops. For anyone still thinking of software as a sidekick, the evidence is hard to ignore: when detection happens at the edge, the software is running the show.
Match the Stage to Your Part, Not the Catalog
Relying on a catalog means treating job descriptions or social scripts as if they were carved in stone. But every stage has its own texture. A role that thrives in a laid-back creative team might suffocate inside a rigid corporate hierarchy. Start by reading the room: what pressure is the team under, what gaps are glaring, and what energy does the moment demand? That tells you more than any generic label ever will.
Take a marketing position as an example. In a two-person startup, the catalog might say "brand manager," but the stage begs for someone who can also run ads, reply to customers, and fix a broken landing page. In a large agency, the same title might mean spending weeks on a single campaign deck. Matching the stage means noticing the difference and choosing where to push your effort, even when it falls outside the neat bullet points.
Ultimately, this is about swapping a fixed identity for a responsive one. Instead of asking, "What should someone in my position do?" ask, "What would move this situation forward right now?" That shift keeps you useful when plans change, which they always do. The catalog is a useful starting point, but the stage writes the real script.
Calibration Drift Over Six Months and What Brands Won't Tell You
Most sensor documentation mentions calibration, but rarely explains how quickly a device can wander from its factory settings. Over six months, even a well-built unit might shift by a few percentage points—enough to turn a 'reliable' reading into a guess. The drift isn't usually a sudden failure; it's a slow accumulation of small environmental stresses, chemical aging, or mechanical fatigue that the internal firmware quietly tries to compensate for.
What brands won't tell you is that many of their recommended calibration intervals are optimistic at best. A six-month window often assumes ideal storage, minimal use, and stable conditions—none of which match real-world operation. By the time the device flags itself as out of spec, you may have already acted on weeks of subtly corrupted data. Some manufacturers even lock the advanced diagnostics behind proprietary software or service plans, making it harder to spot the drift yourself until it's too late.
The practical takeaway is simple: don't wait for a scheduled reminder if your readings start to feel inconsistent or if you've changed how or where the device is used. A quick check against a known reference at the two- or three-month mark costs far less than redoing a batch of work based on questionable numbers. Calibration drift isn't a scandal, but it's also not the rare, negligible event some spec sheets imply.
The Real Cost of a Few Microns Is Not Purchase Price but Process Confidence
When evaluating precision components, the purchase price often dominates the conversation, but in high-stakes manufacturing, a few microns of deviation can quietly erode the entire production line’s reliability. The true cost isn’t found on the invoice; it surfaces later as inconsistent yields, unexpected downtime, or the need for constant recalibration. A lower upfront price means little if the process loses its predictability every time a new batch arrives.
Process confidence is built on repeatability—knowing that the 50th part will fit, measure, and perform exactly like the first. That confidence is hard-won and easily lost when tolerances drift by even a handful of microns. Engineers learn to distrust components that fluctuate near the edge of spec, because the real expense appears in rework, scrap, and the slow erosion of trust in the entire assembly.
Ultimately, the premium paid for a supplier with tight process control isn’t about the metal or the machining time; it’s about buying stability. Fewer surprises on the line, fewer midnight calls about dimensional drift, and the quiet assurance that the next shipment won’t force a process audit. That’s the real value hiding inside those few microns.
FAQ
The gap usually comes down to three things: encoder resolution on the stages, the quality of the edge detection algorithm, and how well the frame handles temperature swings. Mid-range machines often claim 2–3 µm accuracy but struggle below 20°C to 25°C without recalibration. High-end systems use granite bases, air bearings, and sub-pixel interpolation to hold 0.5–1 µm even when the shop floor shifts a few degrees.
Look for manufacturers that build thermal compensation directly into the scale feedback loop. Keyence’s IM series uses a telecentric lens and a vibration-resistant stage that works well next to a press brake. Zeiss O-INSPECT and Mitutoyo Quick Vision also hold tight tolerances in normal shop conditions because their linear encoders are made from zero-expansion glass and the software corrects for residual drift.
A practical range is $45,000 to $120,000 depending on travel and accuracy. If you only need 5 µm on a 300 mm workpiece, a 45k system with manual focus will do. For sub-micron on the same size, expect to pay double. Don’t forget to add 15–20% for fixture plates, ring lights, and the first-year calibration contract.
Software is often the bigger differentiator. Edge detection on a low-contrast plastic part or a burred metal edge can vary by 3–4 µm between brands, even with identical optics. Packages that offer CAD-based comparison, automatic lighting presets, and GD&T evaluation with proper datum simulation will reduce operator error far more than a slightly better camera sensor.
If your tightest tolerance is under 5 µm, the granite and air bearing upgrade pays for itself in stability. Aluminum stages expand with room temperature and develop play after a few million cycles, which shows up as hysteresis in the X-Y plot. Granite with air bearings keeps the stage flat and repeatable for a decade, especially on longer measurements over 200 mm.
Request an on-site acceptance test before signing off. Use a calibrated grid plate or ball bar with features at the extremes of your part size. Measure the same feature 20 times and check the 3-sigma repeatability against the spec sheet. A good vendor will also run a GR&R study with your actual parts, not just a shiny demo block from the showroom.
The three unexpected expenses are software modules (CAD import, SPC reporting, and offline programming are often add-ons), specialized lighting for difficult surfaces, and environmental upgrades like a vibration isolation table or a small air dryer. Also budget for quarterly calibration if your customers require certified traceability, which can run $2,000–$5,000 per year.
Optical resolution matters more for radii under 0.5 mm and chamfer angles, but stage accuracy still influences where that radius sits in space. Pick a machine with at least a 5-megapixel camera and a telecentric lens for edge crispness, then make sure the stage uses linear encoders with 0.1 µm resolution. Rely on sub-pixel algorithms to fill the gap between the two.
Conclusion
A spec sheet showing sub-micron repeatability in a climate-controlled lab tells you almost nothing about what happens on a shop floor where the temperature swings five degrees between morning and afternoon. When a few microns separate a passing part from scrap, you stop caring about catalog numbers and start paying attention to how the machine holds up under real conditions. That means looking for granite stages, thermal compensation sensors, and a brand that publishes drift data instead of hiding it. The stage itself has to match the parts you actually measure: a small, rigid platform for tight medical components is not the same requirement as a long travel bridge for stamped sheet metal. And the software is not an afterthought. Edge detection algorithms differ dramatically in how they handle blur, low contrast, or tilted edges, and that difference shows up directly in repeatability between operators.
Calibration drift is the slow leak most buyers ignore. A machine might pass acceptance testing on day one, but six months later the same reference sphere measures differently. Brands that care will tell you their expected drift rates and recommend intervals without being pushed. The ones that do not are betting you will not check. The true cost of a few microns is rarely the purchase price difference; it is process confidence. When you trust the measurement, you reduce inspection disputes, avoid rework, and stop chasing phantom errors. So when comparing vision measuring machine brands, ignore the headline accuracy and ask instead: how does the system behave on a Tuesday afternoon after a weekend shutdown, with a new operator, measuring a dirty production part? That answer is the precision your parts actually demand.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/